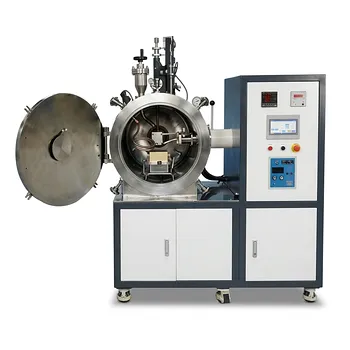
The defining operational characteristics of induction heating sintering immediately set it apart from conventional methods. This process uses a high-frequency alternating current to induce eddy currents directly within a conductive die or sample, achieving total cycle times of 1 to 20 minutes under applied pressures from 10 MPa to 1 GPa. The primary benefits are its exceptionally high heating rates and the ability to concentrate intense thermal power directly into a small sample volume, enabling the rapid consolidation of conductive materials while preserving a fine, homogeneous microstructure.
While conventional sintering is a slow battle against thermal transport limits, the core challenge in induction sintering is mastering electromagnetic coupling. The unparalleled speed and energy efficiency are only achievable when you precisely control the relationship between the magnetic field, the material’s electrical properties, and the applied mechanical force.
Deconstructing the Physics of Speed and Control
The remarkable performance of induction sintering isn't just about applying heat faster. It's a fundamentally different physical mechanism that solves the deep-seated problem of thermal lag in porous powder compacts.
Overcoming Thermal Transport Barriers
A conventional resistance furnace must heat the entire chamber atmosphere, then the crucible, and finally the sample surface through convection and radiation. This is inherently slow and creates thermal gradients.
Induction heating bypasses this bottleneck. The rapidly changing magnetic field generates heat directly within the sample or its electrically conductive container via eddy currents. This volumetric or near-surface heat generation allows the core of a compact to reach the sintering temperature almost as fast as its exterior, eliminating the driving force for differential densification and internal stress.
The Critical Conditions for Efficient Energy Transfer
To transform electromagnetic energy into a perfectly sintered part, you must satisfy three fundamental physical conditions. Failure in any one leads to inefficiency, non-uniform heating, or process failure.
- The Penetration Depth Ratio: The electromagnetic penetration depth (δ) must be less than half the sample's thickness (2δ < d). If the field penetrates too deeply, it passes through the material without inducing sufficient current density for rapid heating.
- Tight Coil-Specimen Coupling: The induction coil must closely match the geometry of the die or sample, and the air gap must be minimal. A loose coupling is like a misaligned gear train—it wastes immense amounts of energy, with efficiency dropping off a cliff.
- Thermal Gradient Avoidance: Unsintered metallic compacts often have high initial electrical resistance. This can cause an "incubation delay" where the sample refuses to heat, followed by a dangerous thermal runaway. The solution is often a two-step process: preheating with radiation or a radio-frequency (RF) field to dramatically reduce resistivity before applying the main high-power sintering stage.
The Five Pillars of Precision in Induction Sintering
When operating a high-temperature induction sintering furnace, the goal is to achieve near-theoretical density without grain growth. This requires orchestrated mastery over five key parameters. These are your primary levers for manipulating the diffusion mechanisms that govern solidifying contraction.
1. Peak Sintering Temperature
The temperature must be high enough to activate the dominant diffusion mechanisms—grain boundary and volume diffusion—that drive densification.
Surface diffusion, which occurs at lower temperatures, only moves mass around pore surfaces without shrinking them. The target temperature must leapfrog this regime into the one where atom movement from grain boundaries fills in pores, causing actual contraction. For conductive powders susceptible to induction, this transition happens rapidly and must be precisely targeted.
2. Sintering Time and Dwell Duration
At the target temperature, time becomes the double-edged sword. A precisely optimized dwell time enables complete pore elimination and robust neck growth between particles.
However, the exceptionally high mobility of atoms in the induction-heated state means that grain boundaries can also move quickly, consuming smaller grains to grow larger ones. The dwell time must be long enough for densification but cut short the moment the pores disappear, before grain coarsening begins. This trades off a few percent of final density for a dramatic gain in mechanical strength.
3. Applied Uniaxial Pressure
Pressure-assisted induction sintering, typically using a graphite die, adds a powerful mechanical driving force alongside the thermal one.
The external load does three critical things: it intensifies particle rearrangement in the initial stage, accelerates the elimination of isolated pores in the final stage by effectively shearing the material around them, and—most importantly—allows you to achieve full density at a lower temperature and in a shorter time. This synergistic effect is the key to beating the grain-size/density trade-off.
4. Atmosphere Control for Surface Chemistry
The vacuum level or inert gas environment (typically argon or nitrogen) in a high-temperature furnace acts as a chemical gatekeeper.
A high vacuum (around 1 × 10⁻³ Torr) is standard for reactive metals to prevent catastrophic oxidation and to pull out volatile impurities and trapped gases during pore closure. In some cases, a partial pressure of an active gas like hydrogen can be used to reduce native surface oxides on powder particles, chemically cleaning the interfaces just as atomic diffusion begins, which dramatically enhances neck growth kinetics.
5. The Role of Sintering Activators
For materials with high melting points or sluggish diffusion, adding a minor sintering activator can fundamentally change the economics of the process.
These additives segregate to particle boundaries and create a high-diffusivity pathway, accelerating shrinkage kinetics at lower temperatures. In an induction furnace, where thermal energy is already concentrated, an activator can lower the required peak temperature by hundreds of degrees, making a previously marginal process window robust and repeatable.
Understanding the Trade-offs and Process Configurations
Induction sintering is not a monolithic solution. The choice of heating mode presents a critical design trade-off that dictates which materials you can process and the ultimate cost of your tooling.
Direct Induction Sintering: Speed with a Prerequisite
In this mode, eddy currents are induced directly within the conductive powder compact itself.
- Primary Advantage: Maximum theoretical heating speed and energy efficiency because there is no intermediary.
- The Deep Need Trade-off: The starting powder compact must have high initial electrical conductivity. Poor initial coupling results in the aforementioned incubation period, and localized hot spots in an inhomogeneous green body can cause catastrophic thermal stress. This mode requires highly controlled, high-purity starting powders.
Susceptor-Assisted Induction Sintering: Flexibility with an Intermediary
Here, a conductive susceptor (typically a graphite die) absorbs the magnetic field and transfers heat to the sample via conduction.
- Primary Advantage: Radical flexibility. Because the sample no longer needs to be electrically conductive, this method can sinter non-conductive ceramics and applies uniaxial pressure uniformly during heating.
- The Deep Need Trade-off: You reintroduce a thermal transfer step. The heating speed is now limited by the thermal conductivity between the susceptor and the sample, and the energy efficiency drops slightly. However, for most applications beyond pure refractory metals, the unparalleled process control this method provides makes it the standard choice.
Making the Right Choice for Your Goal
The decision to deploy induction sintering is a decision to prioritize microstructural control and process speed above all else. Your specific optimization target will dictate how you balance the critical parameters.
- If your primary focus is retaining nano-scale grain size: Maximize the heating rate and apply the highest safe uniaxial pressure. This enables you to drop the peak temperature and reduce the dwell time to a few minutes or even seconds, freezing the microstructure immediately after pore closure.
- If your primary focus is sintering non-conductive ceramics: You must use a susceptor-assisted configuration. Focus your process design not only on the sample but on optimizing the thermal profile of the entire graphite die assembly to ensure uniform radiant and conductive heat transfer to the part.
- If your primary focus is achieving complex, near-net shapes: Direct induction of a loose powder is challenging due to coil geometry constraints. The susceptor-assisted method, with a precisely machined graphite die, allows you to apply isostatic-like densification through uniaxial press tooling, making it the only viable route for engineering components.
The core value of induction sintering is its ability to collapse the time-temperature window of a sintering cycle, giving you direct and immediate command over a material's final microstructure in a way that no conventional radiant furnace can replicate.
Summary Table:
| Parameter / Mode | Core Operational Mechanism | Primary Process Benefit |
|---|---|---|
| Peak Temperature | Activates grain boundary & volume diffusion | Drives rapid densification without unwanted phase shifts |
| Short Dwell Time | Minimizes atom diffusion window post-pore closure | Prevents grain growth, preserving fine microstructures |
| Uniaxial Pressure | Accelerates particle shearing & pore elimination | Achieves full density at lower temperatures & faster cycles |
| Direct Induction | Eddy currents induced directly within conductive sample | Ultra-fast heating rates & maximum energy efficiency |
| Susceptor-Assisted | Indirect heating via conductive graphite susceptor | Versatile processing for non-conductive ceramics & complex shapes |
Elevate Your Material Research with KINTEK Precision Furnaces
Ready to optimize your high-temperature sintering processes and achieve superior material density? KINTEK specializes in advanced laboratory equipment and consumables tailored to your exact research and production demands. We offer a comprehensive range of high-temperature solutions, including induction melting furnaces, vacuum, muffle, tube, rotary, CVD, atmosphere, and dental furnaces—all fully customizable for your unique requirements.
Whether you are refining ceramic sintering protocols or developing novel conductive alloys, KINTEK provides the supply reliability and precise thermal control your team needs. Contact KINTEK today to consult with our laboratory furnace experts and request a tailored quote!
Related Products
- 600T Vacuum Induction Hot Press Vacuum Heat Treat and Sintering Furnace
- Vacuum Induction Melting Furnace
- Vacuum Heat Treat Sintering Furnace with Pressure for Vacuum Sintering
- Vacuum Heat Treat Sintering Furnace Molybdenum Wire Vacuum Sintering Furnace
- Small Vacuum Heat Treat and Tungsten Wire Sintering Furnace
People Also Ask
- Why use Vacuum Hot Press (VHP) for ZnS Ceramics? Achieve Superior IR Transparency and Mechanical Strength
- How does a vacuum hot press sintering furnace mitigate copper sintering swelling? Solve Fe-Cu Expansion Issues
- What are the benefits of using a vacuum hot press sintering furnace for the preparation of SiCw/2024 aluminum matrix composites? Achieve High-Performance Aerospace Materials
- What are the key advantages of vacuum hot press sintering furnaces? Achieve Superior Density and Purity in Materials
- How does the vacuum environment in a vacuum hot press sintering furnace protect chromium-containing ceramics? Find out.