The 3D printer delivers a shaped promise, not a finished part.
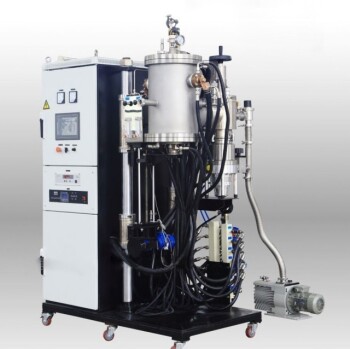
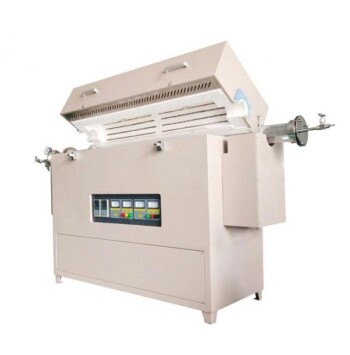
In ceramic Solid Free-Form Fabrication (stereolithography, SLS, FDC, 3DP), the printed “green body” is essentially ceramic powder glued together by a high volume of organic binders, waxes, or monomers. To transform that fragile composite into a dense, structural ceramic, two post-printing thermal steps are non-negotiable: thermal debinding completely removes the organic phase, and high‑temperature sintering fuses the ceramic particles. The required lab furnace must provide precise multi‑stage temperature control, atmosphere management, and uniform gas ventilation to prevent defects and ensure full densification.
Every additively manufactured ceramic part starts as a polymer‑ceramic hybrid. Without meticulously controlled debinding to purge binders and subsequent sintering to eliminate porosity, the component never becomes a true engineering ceramic. The furnace is not an accessory—it is the enabler of material transformation.
The Green Body: A Porous Polymer‑Ceramic Composite
Why printing alone cannot densify the ceramic
Ceramic additive methods use up to 20–40 vol.% of organic binders (methylcellulose, PEG, acrylic resins, waxes) to bind powder during shaping. The resulting green body has little interconnected porosity and holds its form only because of the polymer matrix. The laser or nozzle dwell time is far too brief—typically 0.5 to 25 milliseconds—to achieve the solid‑state diffusion required for particle fusion. The as‑printed part is essentially a highly filled polymer composite, not a ceramic.
The two‑step thermal journey is mandatory
To reach a final dense ceramic, you must first cleanly remove the organic phase without destroying part integrity. Then you must sinter the remaining ceramic skeleton so that particles bond, pores close, and the body shrinks into a hard, strong object. Skipping or rushing either step yields a failed part.
Thermal Debinding: The Delicate Burn‑Out Phase
Why controlled ramp rates are critical
Organic decomposition generates volatile gases that must escape gradually through the powder network. Uncontrolled or rapid heating causes a sudden burst of internal pressure, disrupting particle packing and leading to cracking, blistering, laminations, or bloating. A precise low‑to‑intermediate temperature ramp (often up to ~600 °C) gives binders time to thermally degrade and diffuse out without damaging the ceramic skeleton.
The role of atmosphere and gas flow
Debinding demands continuous gas sweep—whether air for oxidizing binders or inert/reducing gas for sensitive compositions. A furnace with a flowing atmosphere flushes out the decomposition products and prevents residual carbon contamination that can weaken the final ceramic. Capillary extraction (wicking) can remove low‑molecular‑weight waxes early on, but it cannot extract high‑molecular‑weight polymers or isolated pockets left after liquid continuity breaks; thermal burn‑out is the only reliable path to complete binder removal.
Consequences of a rushed debinding
If binders are not fully evacuated before the temperature climbs further, trapped volatiles can carbonize and remain as impurities, or their sudden release during early sintering can create internal pores and stress risers. Staged debinding—with dwells at key decomposition temperatures—ensures the green body becomes a pristine, binder‑free pre‑sintered shape ready for high heat.
High‑Temperature Sintering: Fusing the Ceramic Scaffold
How solid‑state diffusion eliminates porosity
After debinding, the part is a fragile network of ceramic particles with minimal strength. High‑temperature sintering (often up to 1450 °C) provides the thermal energy for solid‑state diffusion and grain growth. Particles bond, open channels close, and the entire body shrinks while densifying by eliminating porosity—transforming the elastic green form into a monolithic ceramic.
Why 3D printing alone can’t sinter
In methods like selective laser sintering, the laser interaction lasts tens of milliseconds, far too short for full atom‑level diffusion. The result is a non‑uniform microstructure, residual stresses, and insufficient densification. Only a post‑process sintering furnace can provide the extended, stable thermal field needed to homogenize the microstructure and achieve the high packing density, strength, hardness, and corrosion resistance expected of a ceramic component.
Maintaining shape through densification
During sintering, the part undergoes controlled shrinkage. A stable, uniform temperature environment preserves the intricate 3D geometry originally imparted by the printing process, preventing warping or slumping even as porosity disappears.
Required Laboratory Furnace Capabilities
Precise multi‑stage temperature control
The furnace must execute programmable ramp‑and‑dwell profiles across two distinct regimes: a gentle debinding ramp (e.g., 0.2–2 °C/min through binder decomposition zones) and a higher‑temperature sintering hold. Without this, you cannot cleanly transition from debinding to densification without defect introduction.
Atmosphere management and gas ventilation
Look for furnaces—atmosphere furnaces, tube furnaces, or muffle furnaces—that allow you to flow air, inert gas, or reducing atmospheres during both stages. Continuous gas sweeps during debinding carry away decomposition products; during sintering, controlled atmospheres prevent oxidation or reduce surface contamination. A static air muffle furnace at 600 °C may suffice for straightforward oxide materials, but reactive or high‑purity ceramics demand sealed atmospheric systems.
Temperature capability and stability
Many oxide ceramics (alumina, zirconia) require sintering temperatures of 1400–1450 °C for full densification. The furnace must reach these levels uniformly, with minimal thermal gradients. Even the debinding phase needs stable control in the 200–600 °C range. Equipment that cannot maintain setpoint stability risks hot spots that cause local melting or incomplete burnout.
Safety and venting
Debinding releases volatile organic byproducts that can condense in the furnace or exhaust. Adequate ventilation, afterburner options, and safety interlocks protect the lab and ensure clean processing.
Understanding the Trade‑offs and Common Pitfalls
Debinding speed vs. defect risk
Faster debinding saves cycle time but dramatically raises the odds of cracks, pores, or blisters. The exact safe rate depends on part thickness, binder formulation, and atmosphere. Thick sections or parts with high binder content need especially slow ramps to allow diffusion out of the core.
Atmosphere choice impacts carbon residue
Oxidizing atmospheres (air) readily burn out many organics, but can also oxidize the ceramic if it’s sensitive (e.g., non‑oxide ceramics). Inert atmospheres prevent oxidation but may leave carbonaceous residue if the gas flow is insufficient to sweep out decomposition products. A balanced approach with precise gas control is key.
Shrinkage and tolerance compensation
Sintering typically brings linear shrinkage of 15–25% or more. The furnace does not control that physically, but a uniform thermal field ensures homogeneous shrinkage; uneven heating causes warping. Designers must pre‑compensate dimensions, and the furnace must deliver the thermal uniformity to faithfully reproduce the scaled‑up geometry.
How to Choose the Right Furnace for Your Ceramic 3D Printing Workflow
Match your furnace capabilities to your material and throughput goals.
- If your primary focus is economical debinding of oxide ceramics (e.g., alumina, 3YSZ): A well‑ventilated muffle or atmosphere furnace with staged ramp control up to ~600 °C is often sufficient for clean burn‑out and can be paired with a dedicated high‑temperature sintering furnace.
- If your primary focus is processing non‑oxide or high‑purity ceramics: Invest in a sealed atmosphere tube or vacuum furnace capable of 1450 °C with programmable multi‑stage ramps and precise gas flow control to prevent oxidation and carbon pickup.
- If your primary focus is research or small‑batch development: Look for benchtop high‑temperature tube or chamber furnaces that offer data logging, multiple atmosphere inlets, and flexible programmability to iterate debinding and sintering profiles safely.
- If your primary focus is production‑scale additive ceramic manufacturing: Consider an integrated furnace system that automates gas switching, provides uniform zone heating, and includes safety features for handling high binder volumes consistently.
The furnace you choose transforms a fragile polymer‑ceramic print into a fully densified, high‑performance component. Invest in the thermal control that your process demands, and you bridge the critical gap between a printed shape and a functional ceramic.
Summary Table:
| Process Stage | Primary Objective | Typical Temp Range | Essential Lab Furnace Capabilities |
|---|---|---|---|
| Thermal Debinding | Cleanly purge organic binders without introducing micro-cracks | 200°C – 600°C | Precise slow-ramp control, continuous gas sweep/ventilation, stable low-temp holds |
| High-Temp Sintering | Drive solid-state diffusion, eliminate porosity & achieve full density | 1400°C – 1450°C+ | High-temp stability, uniform thermal zone, sealed atmosphere/vacuum control |
Transform your ceramic 3D printing workflow from fragile green bodies into fully densified, high-performance components with KINTEK. Specializing in high-temperature laboratory equipment and consumables, KINTEK offers a comprehensive range of customizable furnaces—including muffle, tube, atmosphere, and vacuum furnaces—engineered for precise multi-stage debinding and uniform high-temperature sintering. Eliminate defect risks and achieve optimal material strength today—contact KINTEK's furnace experts now to build your custom thermal processing solution!
Related Products
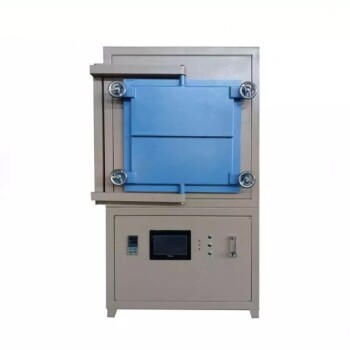
- Laboratory Muffle Oven Furnace with Bottom Lifting
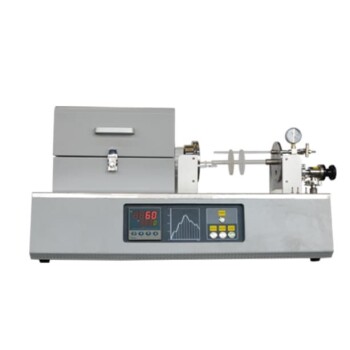
- 1400℃ High Temperature Laboratory Tube Furnace with Alumina Tube
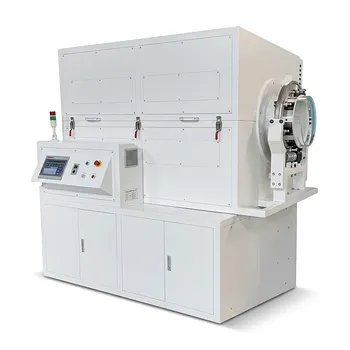
- Laboratory Vacuum Tilt Rotary Tube Furnace Rotating Tube Furnace
- 1200℃ Muffle Oven Furnace for Laboratory
- Laboratory Quartz Tube Furnace RTP Heating Tubular Furnace
People Also Ask
- Why is a high-temperature muffle furnace required for FeOx-MOx/TiO2? Engineering High-Performance Nanocomposites
- What function does a muffle furnace perform in Ba0.75Ca0.25TiO3 calcination? Ensure Phase Purity & Synthesis
- Why is a high-temperature laboratory muffle furnace essential for the alkali fusion process in zeolite synthesis?
- What is the importance of the calcination process? Master High-Purity Calcium Phosphate Nanopowder Production
- What are the primary functions of a high-temperature laboratory muffle furnace in the preparation of biosorbent materials?