Ceramic SLS is not a single-step densification process. Direct laser sintering of crystalline ceramics cannot achieve full density because the laser interaction time—a fraction of a second—provides insufficient thermal energy to drive the solid-state diffusion required for particle fusion. Instead, the laser only melts a sacrificial polymer binder to glue ceramic particles into a fragile “green part,” and true densification only occurs later through prolonged high-temperature furnace post-processing.
Additive manufacturing of technical ceramics demands a two-stage mindset: the printer creates a shaped scaffold, and the furnace delivers the sustained thermal energy necessary to transform that scaffold into a dense, structural ceramic. Without this thermal post-process, you have only compacted powder.
The Fundamental Limitation of Direct Laser Sintering
Why a Laser Cannot Sinter Crystalline Ceramics
During direct laser sintering, a high-power beam scans across a powder bed for a few milliseconds per spot. Crystalline ceramics densify by solid-state diffusion—atoms migrating to eliminate pores and fuse grain boundaries. This diffusion is thermally activated and requires both high temperature and significant dwell time.
The laser simply cannot provide both conditions simultaneously. The thermal pulse is far too short for meaningful atomic movement, so individual ceramic grains never sinter together. Attempts to simply increase laser power lead to thermal shock, cracking, or localized melting that still fails to consolidate the entire part.
The Necessity of a Sacrificial Binder
Because the ceramic itself will not fuse, SLS of ceramics relies on a two-component powder. A sacrificial thermoplastic binder is blended with the ceramic particles, and the laser selectively melts only this binder.
The molten binder wets and connects the ceramic grains, forming a green body with just enough handling strength to be extracted. Crucially, this green body still has low density, high porosity, and zero mechanical integrity for real-world use. The laser has merely “fixed” the shape—not densified the material.
How High-Temperature Furnace Post-Processing Completes the Part
From Green Part to Dense Ceramic in Two Stages
Converting the fragile green part into a fully dense ceramic requires a carefully controlled high-temperature furnace cycle. This cycle is split into two distinct stages: debinding and sintering.
First, the furnace slowly heats the part to a moderate temperature under a controlled atmosphere. During this debinding stage, the polymer binder thermally decomposes and is cleanly removed, leaving behind a purely ceramic, extremely porous “brown” body. Rushing this step traps gas and causes cracks.
After debinding, the furnace ramps to a much higher sintering temperature—often above 70% of the material's absolute melting point. At this stage, solid-state diffusion finally activates, and neck growth between particles closes pores to achieve high density and structural strength.
Why Prolonged Thermal Energy Matters
Dwell time is the key resource a furnace provides that a laser cannot. Atomic diffusion is a rate process governed by temperature and time. By holding the part at an elevated temperature for minutes or hours, the furnace delivers the cumulative thermal energy needed for complete mass transport.
This allows surface curvature-driven driving forces to shrink pores gradually via vacancy diffusion and grain boundary motion. Only through this sustained thermal budget can the ceramic matrix reach the 95–99.9% theoretical density required for load-bearing or transparent applications.
The Flexibility of Modern Laboratory Furnaces
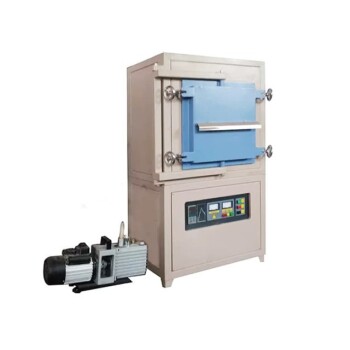
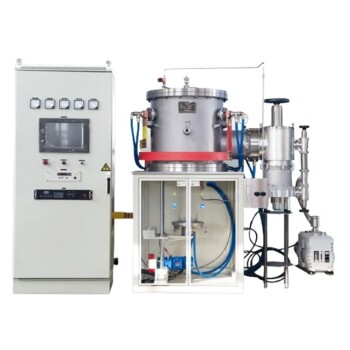
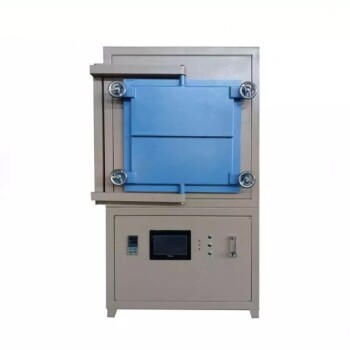
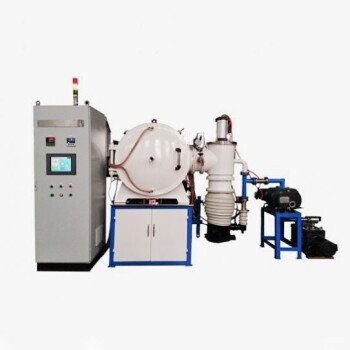
A single furnace push-button process can accommodate various ceramics by adjusting peak temperature, gas environment, and pressure. A muffle furnace handles oxides in air, while a vacuum or controlled-atmosphere furnace prevents undesirable reactions during sintering of non-oxide ceramics like carbides or nitrides.
Some advanced post-processing variants even apply external gas pressure (Hot Isostatic Pressing) or uniaxial mechanical pressure (Hot Pressing) during the thermal cycle. These augment the natural sintering stress to eradicate the last remaining closed pores, achieving theoretical density in materials that resist conventional pressureless sintering.
Understanding the Trade-offs
Shrinkage and Distortion Are Unavoidable
When a green body densifies in a furnace, it shrinks significantly—typically 15–20% linearly. This shrinkage is not always uniform. Constrained regions, non-sinterable inclusions, or thermal gradients inside the furnace can generate internal tensile stresses that retard local densification.
The result is warpage, cracking, or a density gradient if the furnace thermal profile is not perfectly uniform. Designing for predictable, isotropic shrinkage during the CAD-to-part workflow is therefore a critical upfront challenge, and often requires iterative testing with a specific furnace.
High Temperatures Can Trigger Unwanted Grain Growth
The same prolonged high temperature that drives densification also activates grain boundary migration. In ceramics like alumina, pressureless sintering above 1600°C may fully eliminate porosity but cause explosive grain growth that degrades mechanical strength.
This is a classic sintering dilemma: achieving full density purely by time and temperature may sacrifice the fine-grained microstructure that maximizes strength. Advanced methods like two-step sintering, hot pressing, or using dopants to pin grain boundaries attempt to decouple densification from grain coarsening, but they add complexity to the furnace cycle.
Not All Porosity Can Be Removed with Heat Alone
During the final stage of conventional sintering, closed pores become isolated from grain boundaries. With no short-circuit diffusion path, the driving force for their removal plummets. Even after many hours, a small volume fraction of residual pores remains.
This residual porosity scatters light severely, preventing transparency, and acts as fracture origins. Solving this last-pore problem often requires switching from simple atmospheric furnace sintering to pressure-assisted processes (HIP or hot pressing), which introduce an extra driving force that heat alone cannot provide.
How to Apply This to Your SLS Workflow
If you are developing or working with ceramic SLS, the printing step is only the beginning. Your decision-making must shift the focus to post-processing as the true shaping and property-defining operation.
- If your primary focus is mechanical strength: Never skip the high-temperature furnace cycle. Use a full debinding-and-sintering profile with sufficient dwell time to close interconnected porosity, and consider hot isostatic pressing if a fully dense, flaw-free part is required.
- If your primary focus is minimizing distortion: Invest in precise furnace temperature control and uniform heating rates. Design green parts with oversized dimensions, incorporate settling geometries, and use substrates or setters that match the shrinkage coefficient of your ceramic.
- If your primary focus is a fine-grained microstructure: Avoid the highest sintering temperatures that trigger rapid grain coarsening. Explore lower-temperature liquid-phase sintering or pressure-assisted furnaces that push density to the finish line before grains have time to grow.
- If your primary focus is optical transparency: Understand that pressureless furnace sintering alone will almost always leave a haze of residual pores. You must follow a two-step furnace strategy: conventional sintering to close open porosity, then a hot isostatic pressing furnace to collapse the last isolated pores.
The printer gives you geometry; the furnace gives you a ceramic. By respecting the underlying diffusion physics and choosing the right thermal post-processing path, you bridge the gap between a fragile green form and a fully dense, high-performance component.
Summary Table:
| Stage / Parameter | Laser Sintering (SLS) | Furnace Post-Processing |
|---|---|---|
| Primary Mechanism | Sacrificial binder melting (millisecond pulse) | Solid-state atomic diffusion (prolonged thermal dwell) |
| Resulting Structure | Fragile "Green Part" with low density | Fully dense ceramic (95–99.9% theoretical density) |
| Primary Function | Shapes complex part geometry | Cleans binder (debinding) & eliminates pores (sintering) |
| Material Strength | Zero mechanical structural integrity | High mechanical strength, wear, & temperature resistance |
Ready to transform your 3D-printed ceramic green parts into high-performance structural components? KINTEK specializes in advanced laboratory equipment and customizable high-temperature furnaces—including muffle, tube, vacuum, controlled-atmosphere, CVD, and induction melting furnaces—engineered to provide the precise temperature control and uniform heating required for critical debinding and sintering cycles.
Don't let inadequate post-processing compromise your ceramic properties. Contact KINTEK today to consult with our thermal processing experts and find the ideal high-temperature furnace for your laboratory or production workflow!
Related Products
- 1400℃ High Temperature Laboratory Tube Furnace with Alumina Tube
- 1800℃ High Temperature Muffle Oven Furnace for Laboratory
- 1700℃ High Temperature Laboratory Tube Furnace with Alumina Tube
- 1700℃ High Temperature Muffle Oven Furnace for Laboratory
- 1700℃ Controlled Inert Nitrogen Atmosphere Furnace
People Also Ask
- How are high-temperature laboratory tube furnaces applied in long-term vacuum homogenization heat treatments for intermetallic samples?
- How do high-temperature laboratory tube furnaces ensure environmental stability? Precision Thermal Reduction Tips
- How are high-temp tube furnaces used to measure diffusion coefficients per Fick's law? Master Precision Annealing
- How are high-temperature tube furnaces applied in testing ceramic-supported alloy membranes? Insights
- What is the mechanism of a high-temperature furnace in Bi-2223 sintering? Achieve Precision Phase Transformation