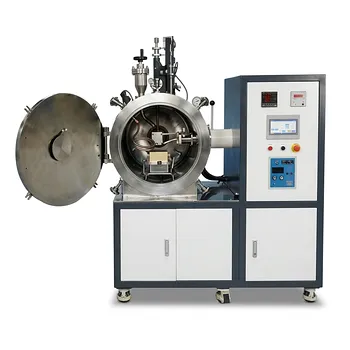
The multi-component binder system is the architect of the entire thermal debinding and sintering cycle.
In Ceramic Injection Molding, the interplay of a major polymer binder, a minor wax-based binder, and processing aids directly dictates every hold temperature, ramp rate, and atmosphere choice in downstream furnaces. The minor binder must decompose first to create an open network of pores, allowing the later breakdown gases of the major binder to escape without cracking or blistering the part. As a result, furnaces require multi-segment programmable controllers and tightly regulated inert or vacuum environments—requirements that flow not from generic best practice, but from the specific chemistry of the feedstock.
The multi-stage nature of CIM binder burnout is not a flexibility—it’s a rigid structural demand. The minor binder volatilizes at low temperatures and physically carves out escape channels. This dictates a thermal profile with precise low-temperature holds and demands an atmosphere that can safely evacuate up to 40 vol.% of organic additives without oxidizing the ceramic powder. Failure to respect this sequence means catastrophic defects.
Why Sequential Binder Removal is Critical
The Minor Binder: Opening the Escape Routes
The minor binder—typically a paraffin wax or similar low-molecular-weight compound—is designed to volatilize or pyrolyze at relatively low temperatures, often between 150°C and 300°C. This initial decomposition creates an interconnected open porosity network throughout the green part, establishing the pathway for all subsequent gas evolution. Without this step, the part remains sealed and any gas generated later will be trapped.
The Major Binder: Escaping Without Damage
The major binder, such as polypropylene or polyethylene, requires higher temperatures (300–500°C) to break down. Because the open pore channels already exist, the gaseous decomposition products can freely migrate to the surface and be swept away. If the minor binder had not left first, the resulting internal pressure would cause cracking, blistering, or slumping that renders the component unusable.
The Role of Processing Aids
Components like plasticizers and lubricants also volatilize across specific temperature ranges. Their removal is integrated into the thermal schedule, but the fundamental framework remains the staged, sequential sacrifice of the minor binder before the major binder. This chemical order of operations is non-negotiable.
How Binder Chemistry Directs the Thermal Profile
Multi-Segment Heating Ramps
A multi-segment programmable temperature controller is not just a convenience—it is the only way to execute the required sequence. The furnace must ramp slowly to a first debinding hold at the minor binder’s decomposition range, dwell for a precisely defined period, then ramp to one or more higher holds for the major binder. Skipping or shortening these holds invites disaster.
Low-Temperature Precision is King
The most critical phase of the entire process often occurs between 150°C and 400°C. Here, even small temperature deviations can accelerate decomposition too rapidly or leave binder residues that cause problems later. High-temperature laboratory furnaces designed for CIM must therefore exhibit exceptional temperature uniformity and control fidelity in a range that many sintering furnaces treat as an afterthought.
From Debinding to Sintering
After complete thermal removal of the organic components—often 30–40% of the initial volume—the fragile brown part remains, held together only by weak interparticle friction. The same furnace (or a downstream unit) must then execute a high-temperature ramp to ceramic sintering temperatures (e.g., 1500°C–2000°C) without disturbing the particle packing or allowing any residual vapor to disrupt densification.
Atmosphere Control: Why It’s Non-Negotiable
Inert and Vacuum Environments
Most CIM formulations use oxygen-sensitive non-oxide powders such as silicon nitride, silicon carbide, or aluminum nitride. Exposing these materials to air during binder burnout would cause oxidation and ruin the final properties. Therefore, inert atmospheres (argon, nitrogen) or vacuum are mandatory to cleanly decompose the organic binder without contaminating the ceramic matrix. Even for oxides, an inert sweep prevents carbonaceous residues that could interfere with sintering.
Reducing Atmospheres and Safety Boundaries
In some cases, a hydrogen-bearing reducing atmosphere is used to remove carbon residues or to reduce stubborn oxides, leaving only the desired ceramic. Hydrogen, however, requires substantial safety interlocks, burn‑off stacks, and explosion‑proof construction. This can dramatically influence furnace design and the economics of whether to combine debinding and sintering in a single unit.
Gas Flow and Sweep Dynamics
Effective binder removal is not just about chemistry—it’s about transport. The furnace must provide controlled gas flow to carry decomposition products away from the part and out of the hot zone. Stagnant gas pockets can lead to re‑condensation of waxes or create localized overpressure, once again risking cracks. Mass flow controllers and active exhaust management become indispensable.
Understanding the Trade-offs and Practical Pitfalls
Single Furnace vs. Separate Debinding and Sintering Units
When the process atmosphere is fully inert (vacuum, argon, nitrogen), a debinding furnace can be significantly cheaper than a high-temperature sintering furnace. This cost difference often justifies using two separate units, freeing the expensive sintering furnace from long, low-temperature cycle times. However, if the process demands flammable hydrogen, the safety measures needed make the cost gap shrink, and the logistical benefits of a single combined furnace may become the deciding factor.
Binder Residue: A Deliberate or Detrimental By‑product
The polymer system leaves more than porosity. As demonstrated in powder injection molding, using high-density polyethylene (HDPE) as the major binder can leave a uniform dispersion of fine TiO₂ ash (~0.2 µm) after burnout in hydrogen. This residue, if carefully managed, can actually promote smoother, more complete sintering by coating particle surfaces. In CIM, the choice of binder chemistry must account for whether such trace residues are beneficial or must be eliminated entirely—another demand placed on the furnace atmosphere and thermal profile.
Cycle Time Bottlenecks
Debinding is inherently slow; pushing it too fast leads to defects. Because debinding often consumes more total furnace time than sintering, a process bottleneck can form. This reality pushes manufacturers to carefully weigh throughput when deciding between one‑furnace and two‑furnace strategies, especially when scaling from prototype to production.
Making the Right Choice for Your Furnace Strategy
The design of your debinding and sintering equipment must trace back to the exact binder chemistry you use. Align your approach with your materials and production goals.
- If your primary focus is non‑oxide ceramics (e.g., Si₃N₄, SiC): Prioritize a furnace with full vacuum/inert gas capability and multi‑segment programming to prevent even trace oxidation during the long debinding stage.
- If your primary focus is oxide ceramics that tolerate air burnout: A simpler air‑atmosphere muffle furnace can suffice for debinding, but you still require staged heating holds to avoid cracking.
- If your process relies on hydrogen for residue control: Carefully compare the total cost of separate vs. combined furnaces—safety upgrades often narrow the price gap, making a single combined unit viable and simpler to operate.
- If you are scaling up production: Consider a dedicated debinding furnace to free expensive sintering capacity, as low‑temperature burnout cycles are the primary bottleneck; the increased throughput often justifies the extra equipment.
- If you encounter blistering or cracking in current parts: Examine your thermal profile first—ensure a clear low‑temperature hold exists at the minor binder’s decomposition range, and verify that gas flow rates are sufficient to evacuate decomposition products without turbulence.
By accepting that each binder component writes a specific chapter of the thermal profile, you stop treating your furnace as a generic oven and start using it as the precise, chemistry‑driven instrument that ceramic injection molding truly demands.
Summary Table:
| Process Phase | Temperature Range | Primary Function & Mechanism | Essential Furnace Requirement |
|---|---|---|---|
| Minor Binder Removal | 150°C – 300°C | Volatilizes wax/additives to form an interconnected open pore network | High low-temp precision, multi-segment holds, active gas sweep |
| Major Binder Removal | 300°C – 500°C | Decomposes polymer backbones; gases escape via pre-formed pores | Controlled ramp rates, inert/vacuum/H₂ atmosphere, exhaust management |
| Ceramic Sintering | 1500°C – 2000°C | Densifies the fragile 'brown part' into final high-strength ceramic | Ultra-high temperature capacity, strict vacuum/inert atmosphere control |
Master Your CIM Thermal Processing with KINTEK
Don't let improper binder burnout cause cracking, blistering, or process bottlenecks in your advanced ceramic production. KINTEK specializes in high-performance laboratory equipment and high-temperature furnaces—including muffle, tube, rotary, vacuum, atmosphere, and combined debinding-sintering units—engineered for precise multi-segment temperature control and advanced atmosphere management.
Whether you work with non-oxide ceramics requiring strict inert environments or need tailored, customizable furnace solutions to optimize throughput, our experts are here to help.
Contact KINTEK today for a customized furnace solution to ensure defect-free CIM components and elevate your laboratory efficiency!
Related Products
- High Temperature Muffle Oven Furnace for Laboratory Debinding and Pre Sintering
- Chairside Dental Porcelain Zirconia Sintering Furnace with Transformer for Ceramic Restorations
- Dental Porcelain Zirconia Sintering Ceramic Vacuum Press Furnace
- Vacuum Dental Porcelain Sintering Furnace for Dental Laboratories
- Custom Made Versatile CVD Tube Furnace Chemical Vapor Deposition CVD Equipment Machine
People Also Ask
- What thermal phenomena occur during polymer binder burnout in ceramic green bodies? Lab Furnace Guide
- Why is controlled heat treatment in a muffle furnace necessary for calcined clay? Achieve Optimal Pozzolanic Activity
- What role does a high-temperature muffle furnace play in STFO synthesis? Achieve Pure Perovskite Results
- How does a high-temperature muffle furnace facilitate the formation of LaNbxAl1−xO3+δ perovskite structures? Key Roles
- What role does a high-temperature muffle furnace play in the formation of biochar catalysts? Master Catalyst Synthesis